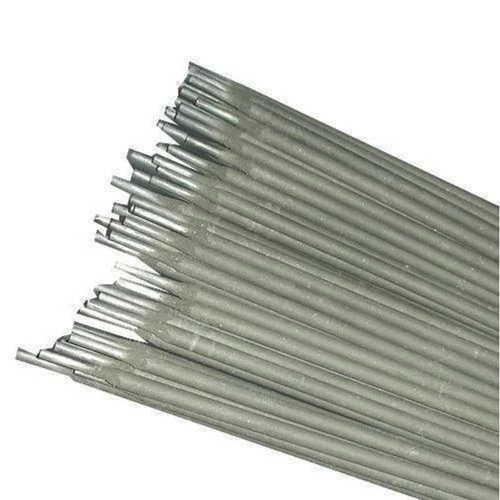
Low Hydrogen Electrodes
Crack-Resistant High Tensile Welding
Low hydrogen electrodes (E7018 type) are used for welding high-tensile and alloy steels where hydrogen-induced cracking must be avoided. They require pre-drying before use to maintain low moisture content.
Chemical Composition & Mechanical Properties
Swipe sideways to see all columns
| Electrode Type | C % | Mn % | Si % | S % Max | P % Max | Other Elements | Tensile Strength (N/mm²) | Yield Strength (N/mm²) | Elongation % | Impact (CVN) |
|---|---|---|---|---|---|---|---|---|---|---|
| Low Hydrogen Electrodes | ||||||||||
| E7015 | 0.10 max | 1.25 max | 0.90 max | 0.03 max | 0.03 max | Ni=0.30max, Cr=0.20max, Mo=0.30max, V=0.080max, Mn+Ni+Cr+Mo+V=1.50max | – | 400 min | 24-30 | 20°C 120-200J; 20°C 100-180J; -20°C 80-160J; -30°C 60-140J |
| E7016 | 0.10 max | 0.8-1.60 | 0.75 max | 0.03 max | 0.03 max | Ni=0.30max, Cr=0.20max, Mo=0.30max, V=0.080max, Mn+Ni+Cr+Mo+V=1.75max | 510-610 | 440-540 | 24-30 | 27°C 120-210J; 0°C 100-180J; -20°C 90-160J; -29°C 50-125J |
| E7016-1 | 0.10 max | 1.0-1.60 | 0.60 max | 0.025 max | 0.025 max | Cr=0.20 max, Ni=0.30 max, Mo=0.30 max, V=0.080 max, Mn+Ni+Cr+Mo+V=1.75max | 500 min | 400 min | 24 min | -46°C 90J |
| E7018 | 0.10 max | 0.8-1.60 | 0.75 max | 0.03 max | 0.03 max | Ni=0.30max, Cr=0.20max, Mo=0.30max, V=0.080max, Mn+Ni+Cr+Mo+V=1.50max | 510 min | 440 min | 24-30 | 20°C 120-200J; 0°C 100-180J; -20°C 80-160J; -30°C 60-140J |
| E7018-1 | 0.10 max | 1.0-1.60 | 0.45 max | 0.025 max | 0.025 max | Ni=0.30max, Cr=0.20max, Mo=0.30max, V=0.080max, Mn+Ni+Cr+Mo+V=1.50max | 500-600 | 440-540 | 24-30 | -46°C 50-150J; -50°C 50-120J |
| E7018-1 | 0.09 max | 0.90-1.40 | 0.15-0.50 | 0.012 max | 0.015 max | Ni=0.30max, Cr=0.20max, Mo=0.30max, V=0.080max, Mn+Ni+Cr+Mo+V=1.75max | 500-610 | 425-540 | 24-32 | -46°C 40-120J |
| E7024 | 0.04-0.12 | 0.45-0.85 | 0.25-0.45 | 0.035 max | 0.035 max | Ni=0.30 max, Cr=0.20 max, Mo=0.30 max, V=0.080 max | 500-600 | 430-520 | 22-28 | 0°C 48-88J |
| E7014 | 0.10 max | 1.25 max | 0.90 max | 0.03 max | 0.03 max | Ni=0.30 max, Cr=0.20 max, Mo=0.30 max, V=0.080 max | 510-600 | 430-500 | 22-28 | 0°C 47-88J |
Very low hydrogen content reduces cracking risk
High tensile strength weld deposits
Excellent impact resistance at low temperatures
Smooth, dense weld bead with minimal porosity
Suitable for critical structural applications
More in Welding Electrodes
You May Also Need
Popular picks from our other product categories
Reasons to Buy From Dilipkumar & Associates
60+ Years Industry Legacy
Established presence in the welding industry with decades of market experience and deep manufacturer relationships.
Authorised Dealer & Stockist
Official supply partner for India's most recognised welding brands — guaranteed genuine products.
Wide Product Range
Comprehensive availability of welding consumables, machines, accessories, and safety equipment under one roof.
Ready Stock Availability
Maintains strong inventory to support both urgent requirements and scheduled industrial procurement.
Dependable Service
Structured supply processes focused on timely delivery and responsive customer support.
Strong Industry Relationships
Long-standing partnerships with manufacturers, contractors, and industrial customers across the region.
Have Questions About Low Hydrogen Electrodes?
Our team can confirm pricing, availability, and technical specifications for your requirement.